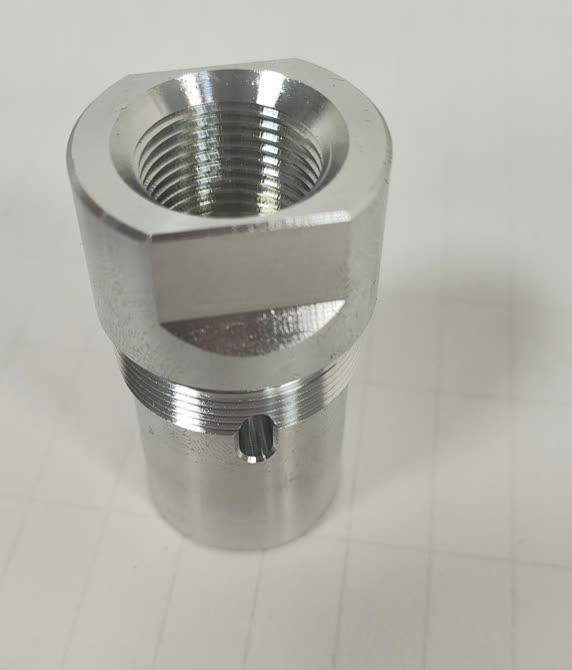
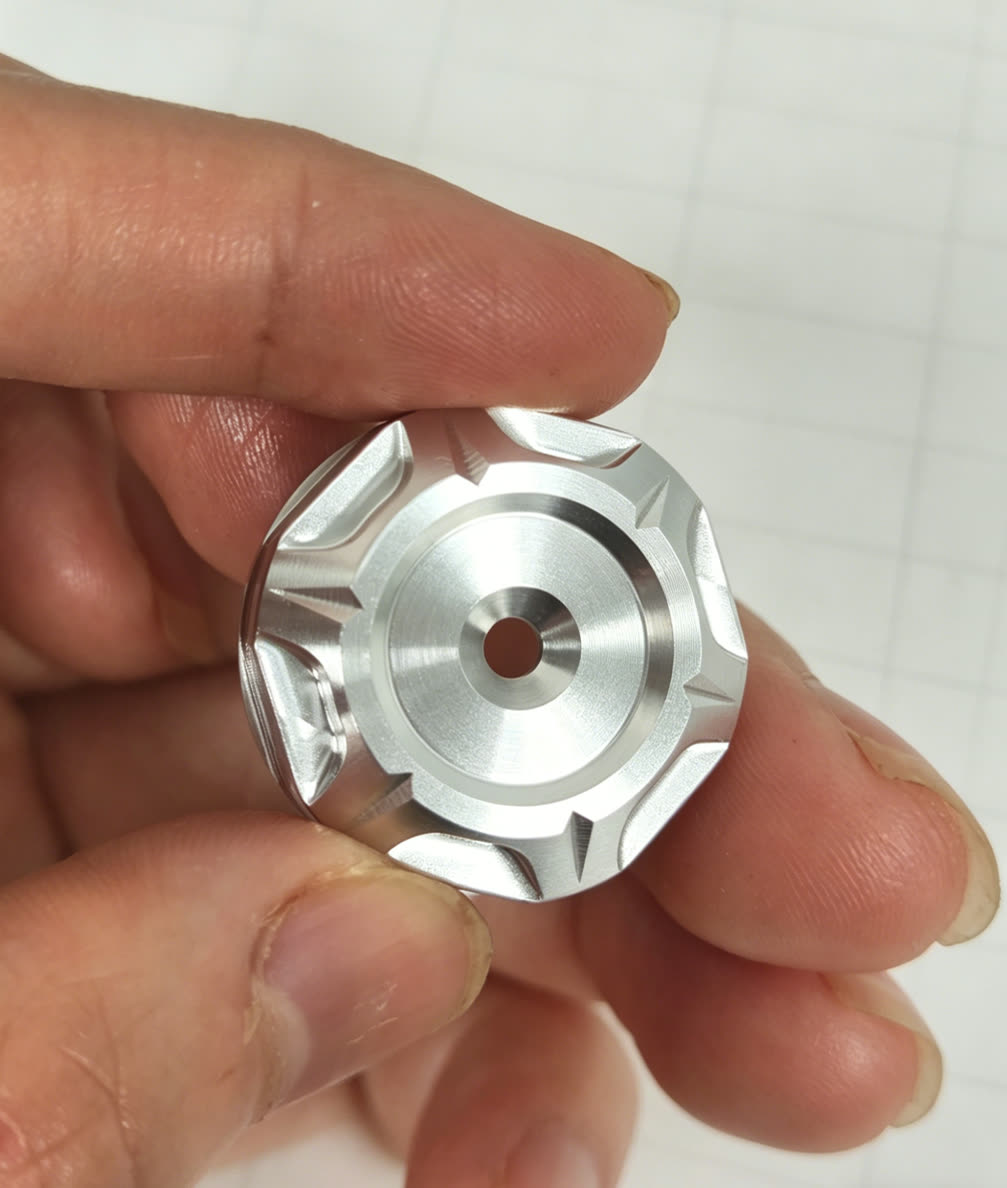
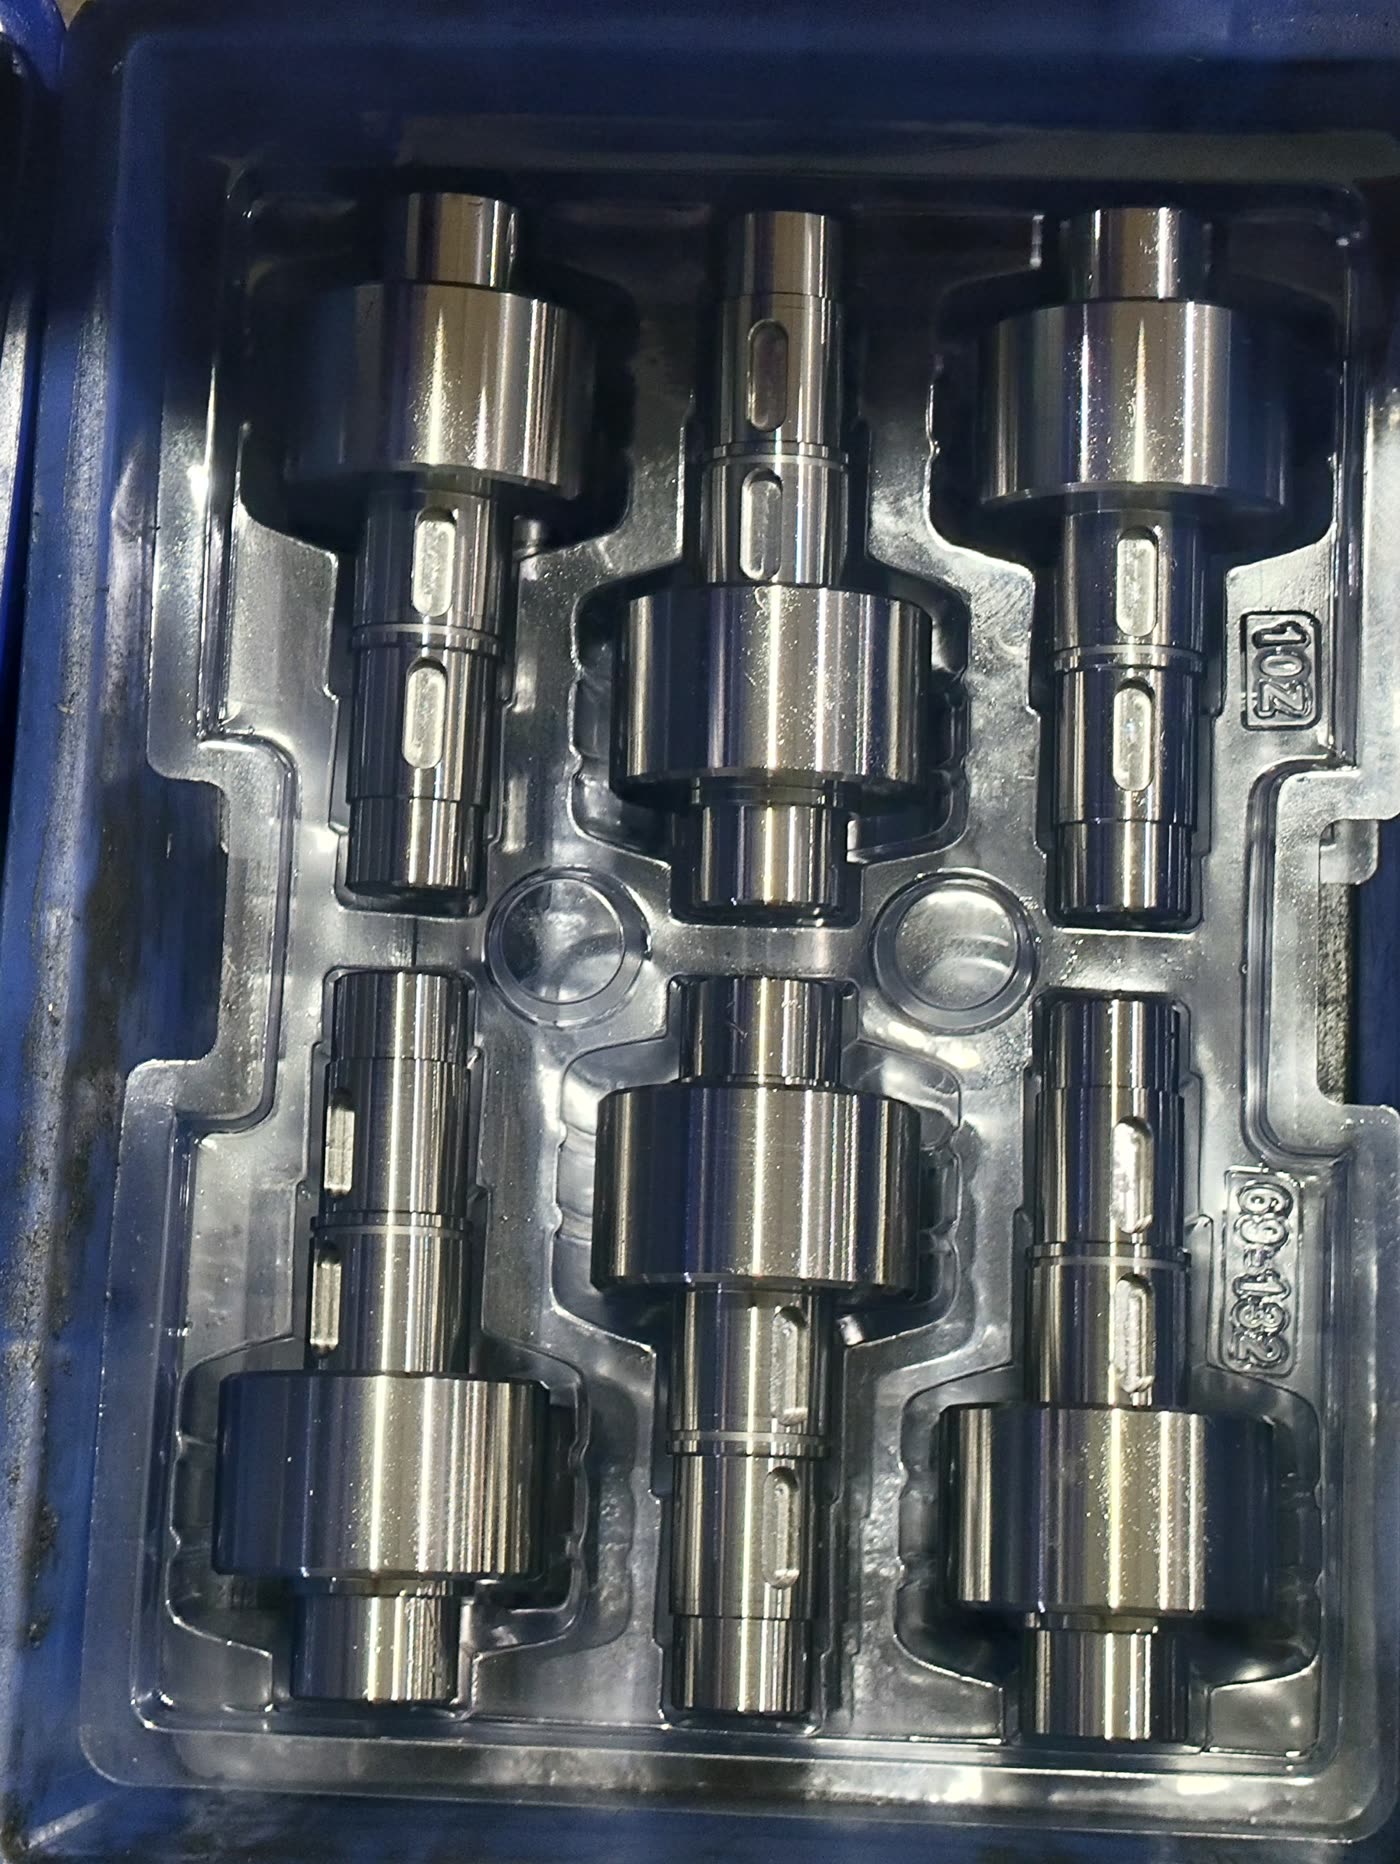
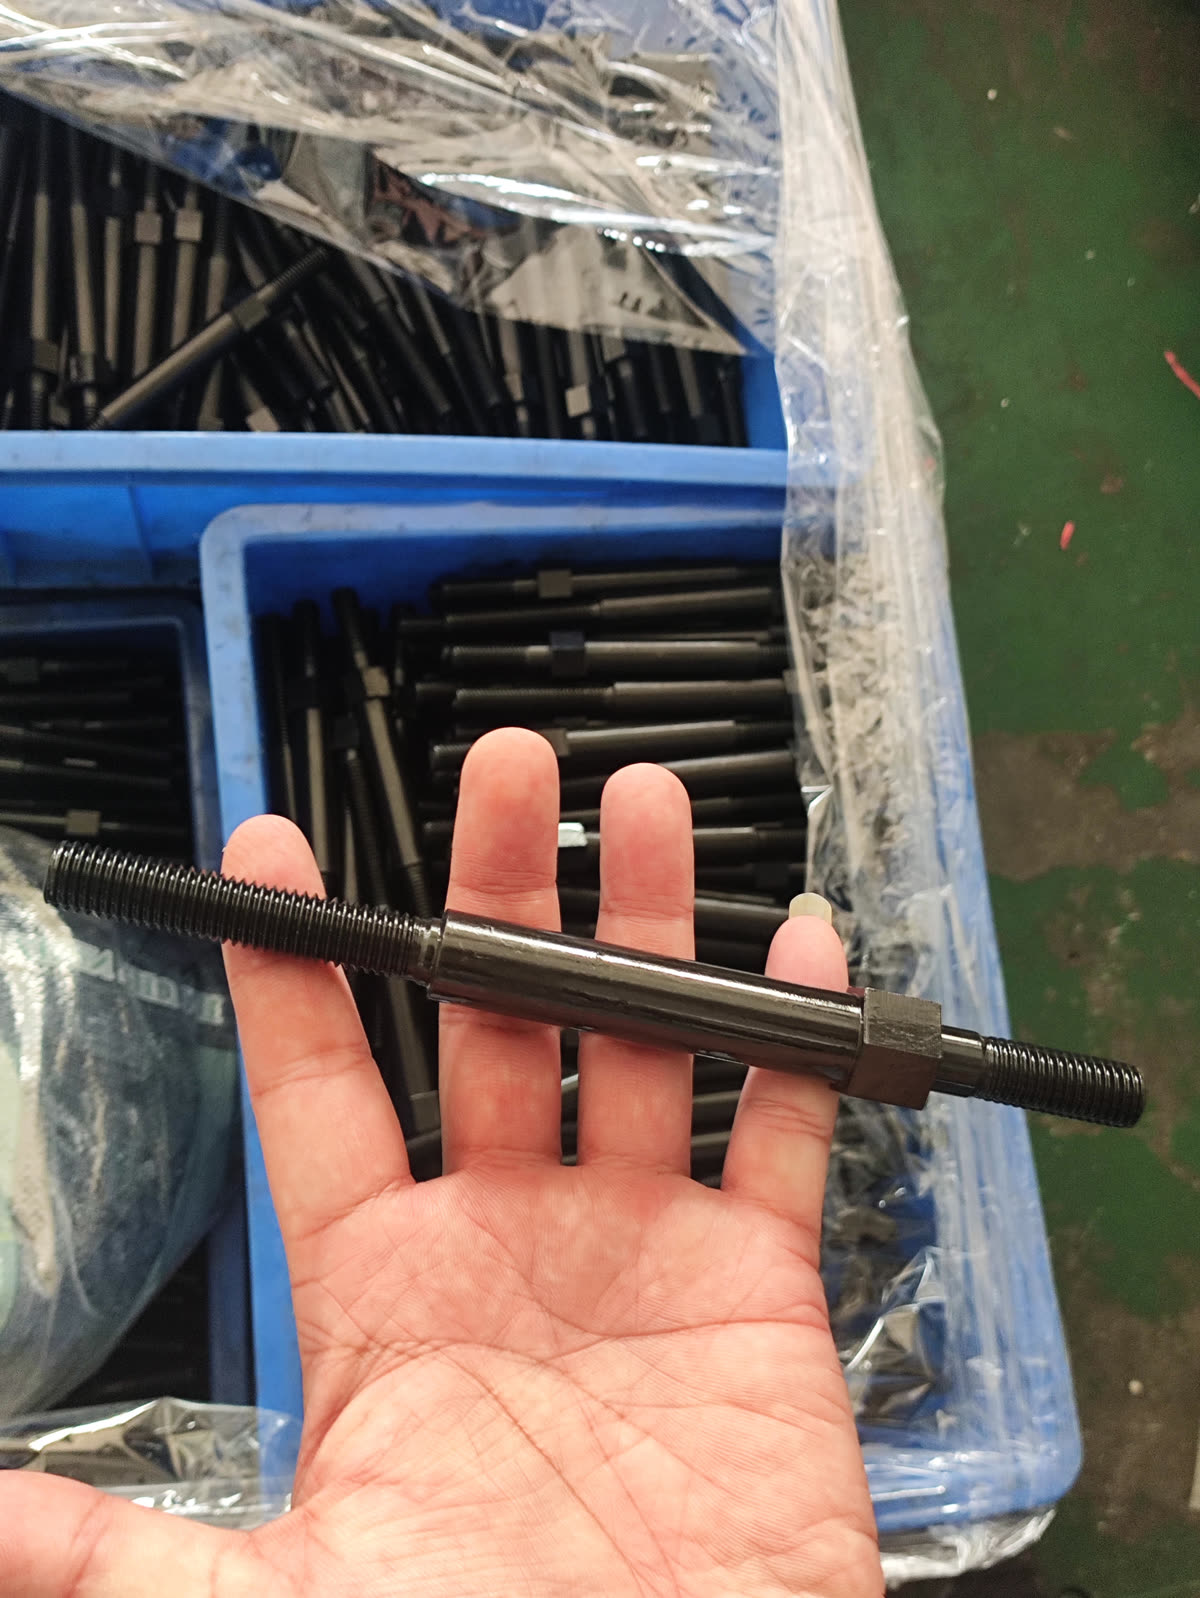
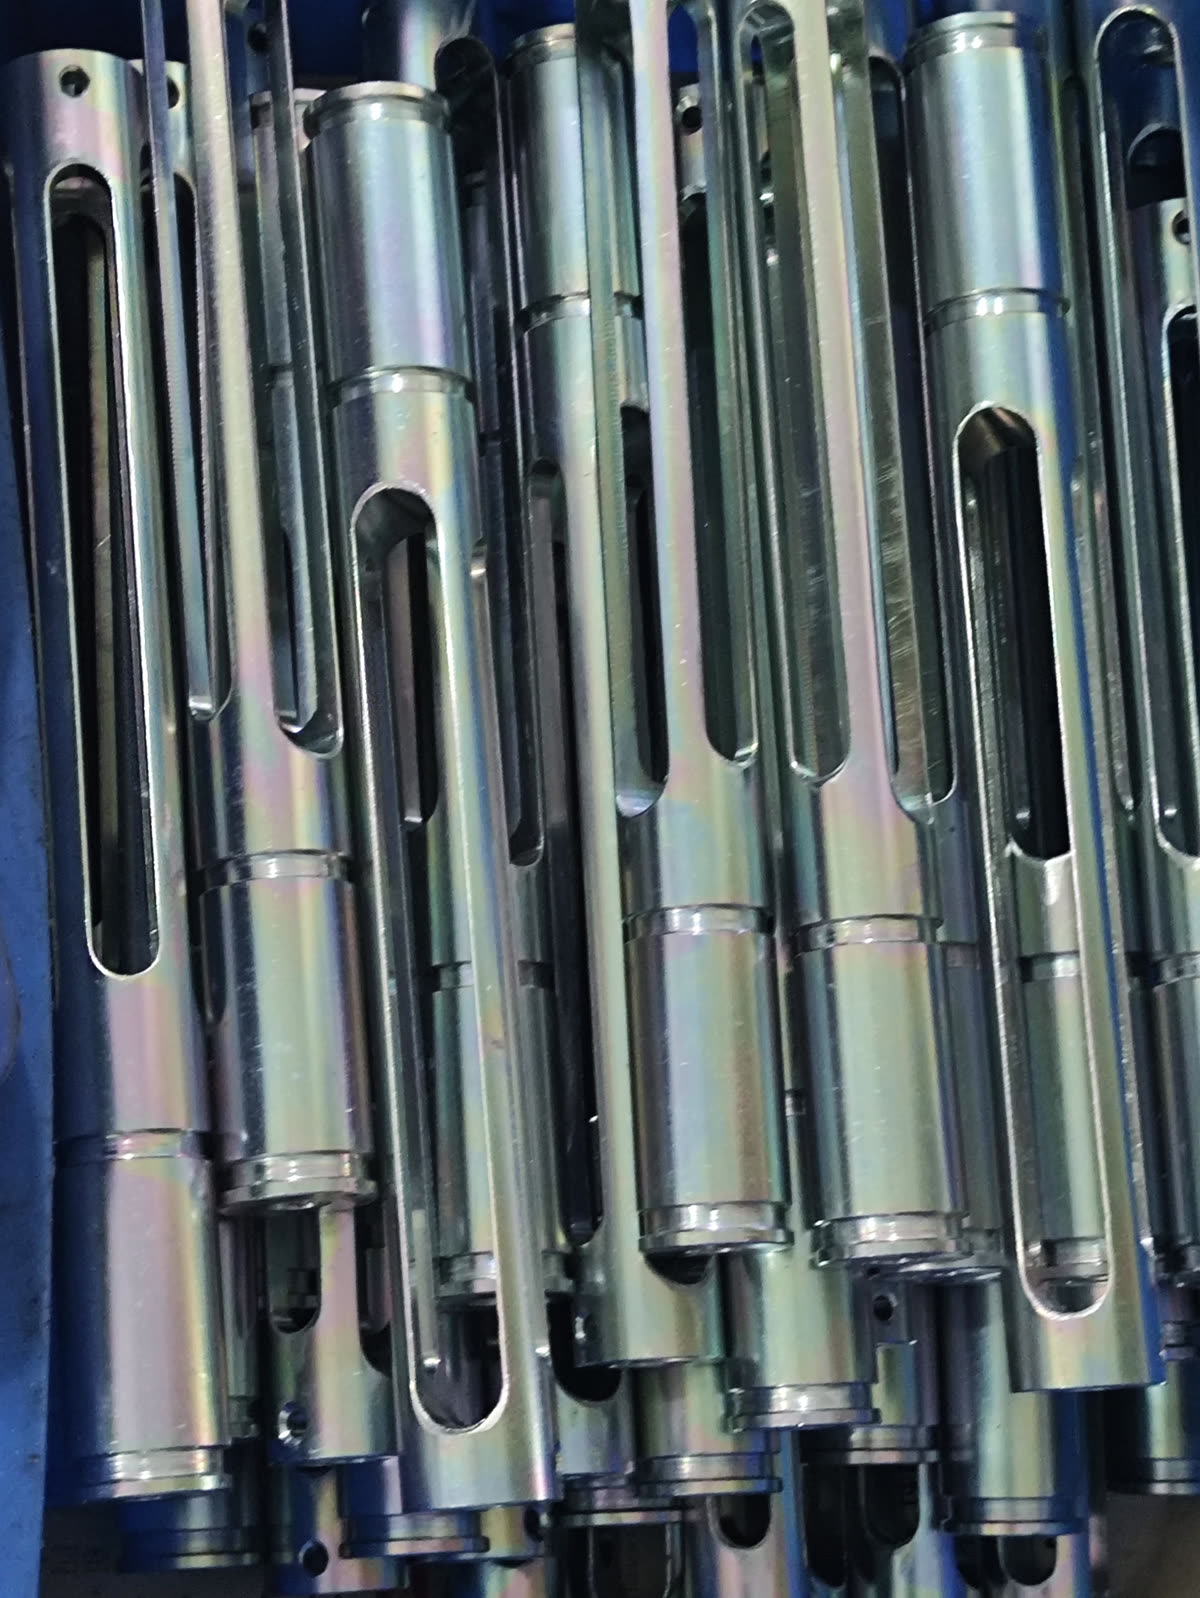
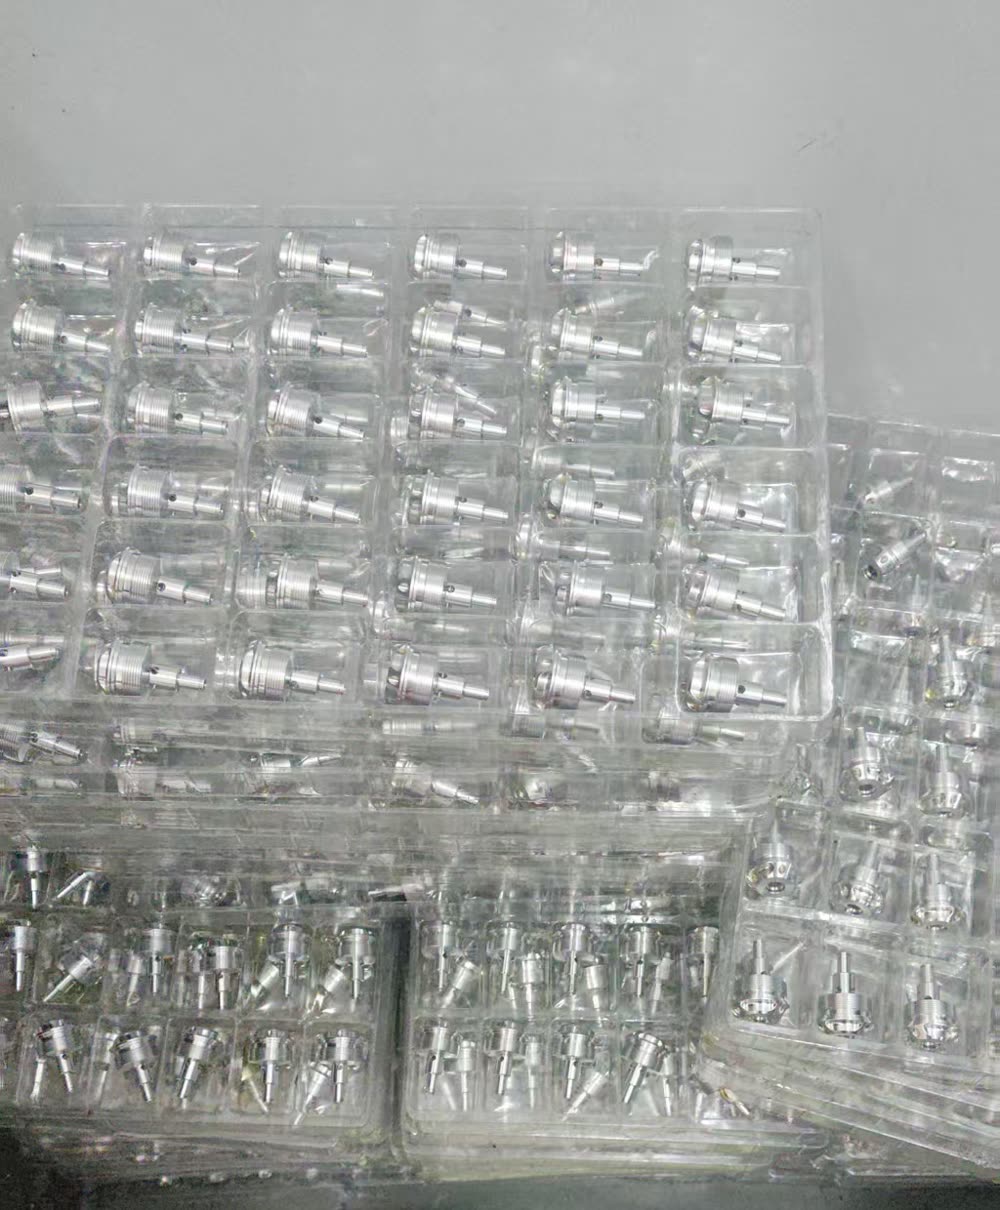
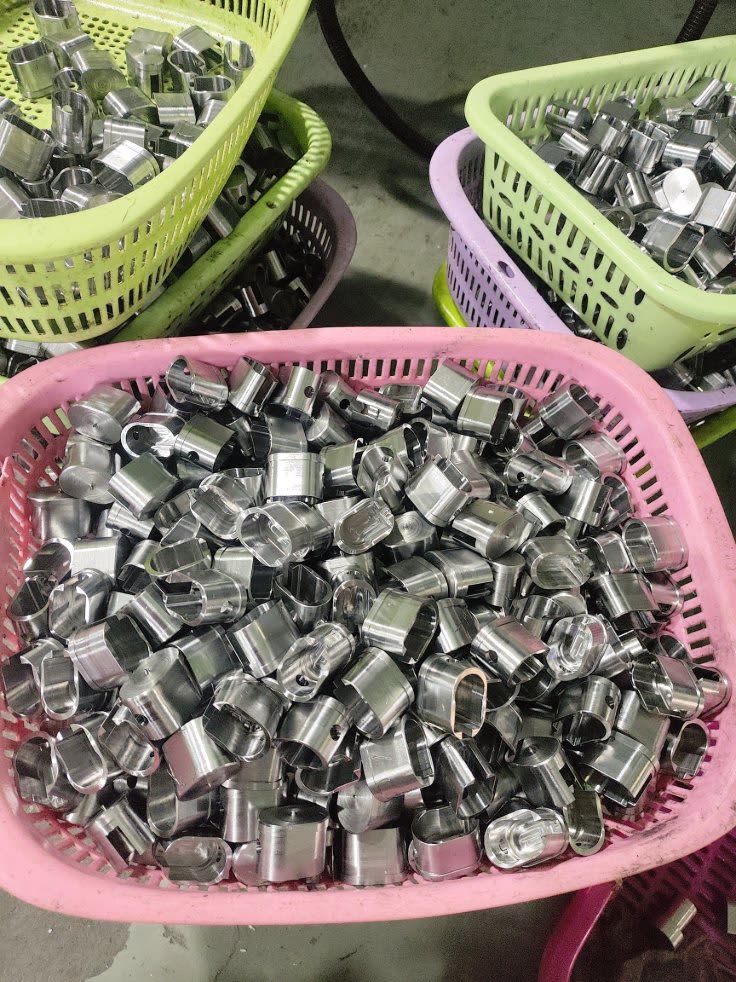
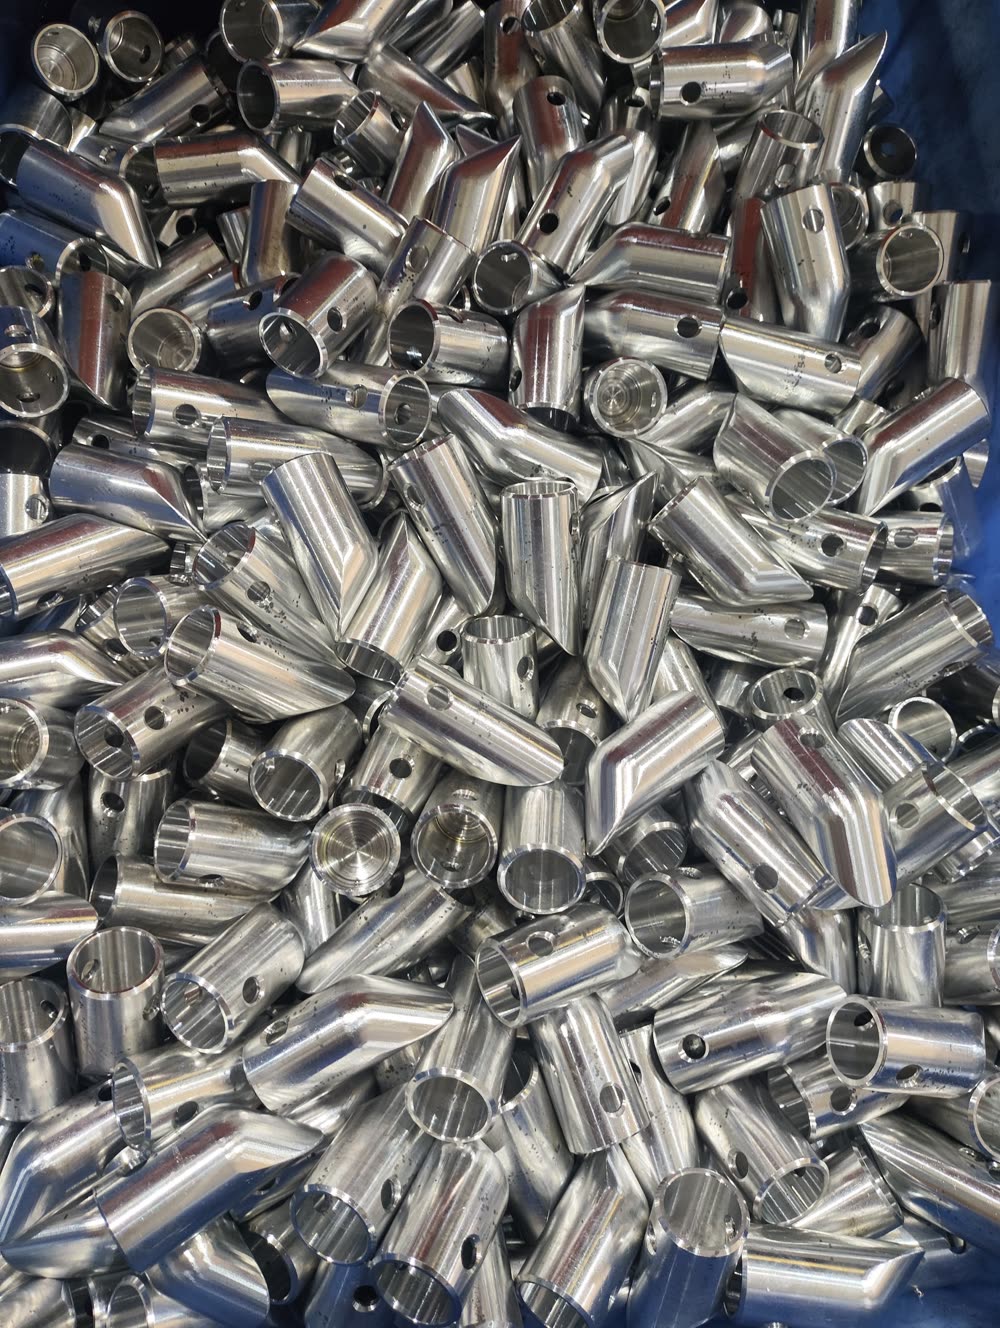
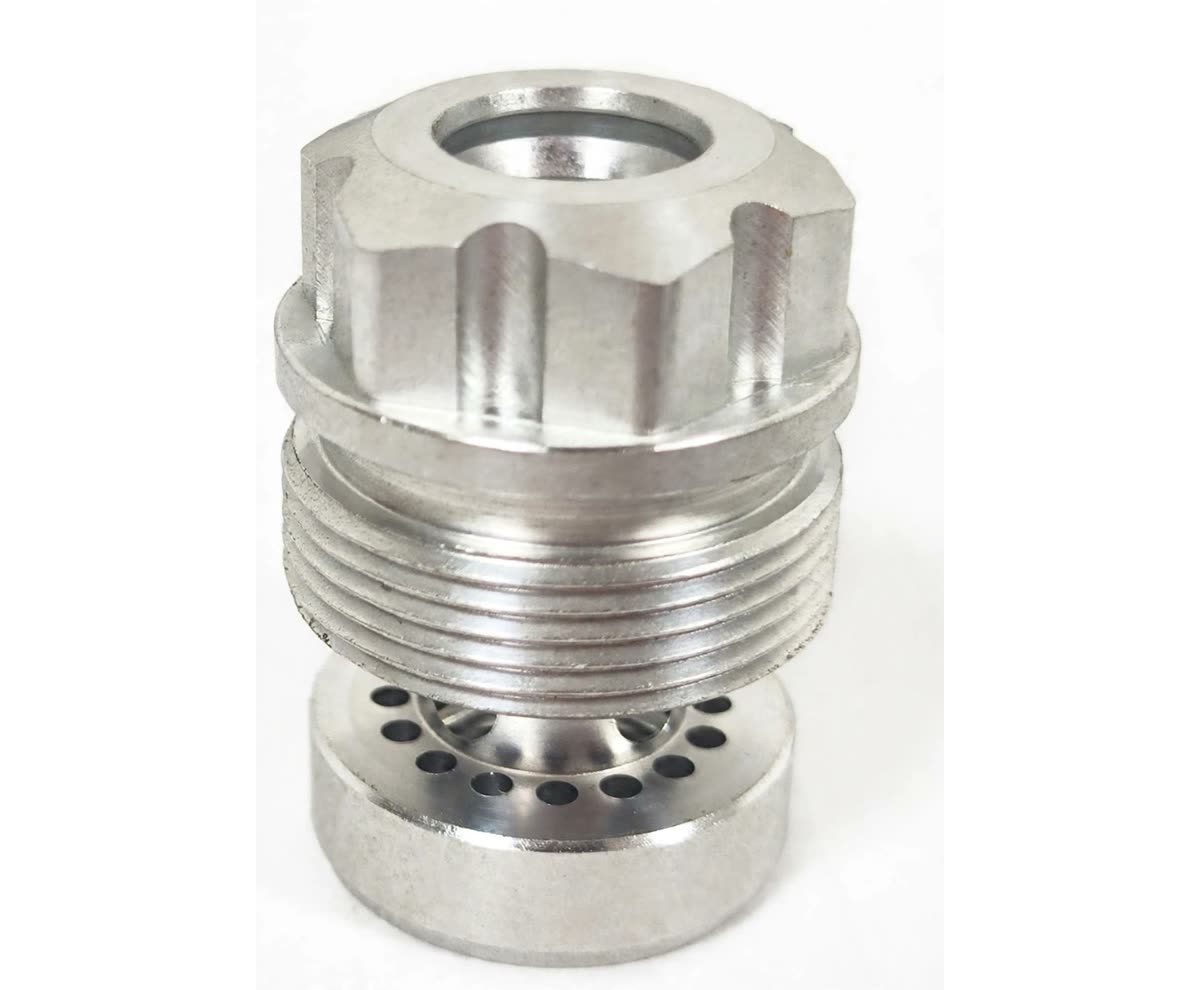
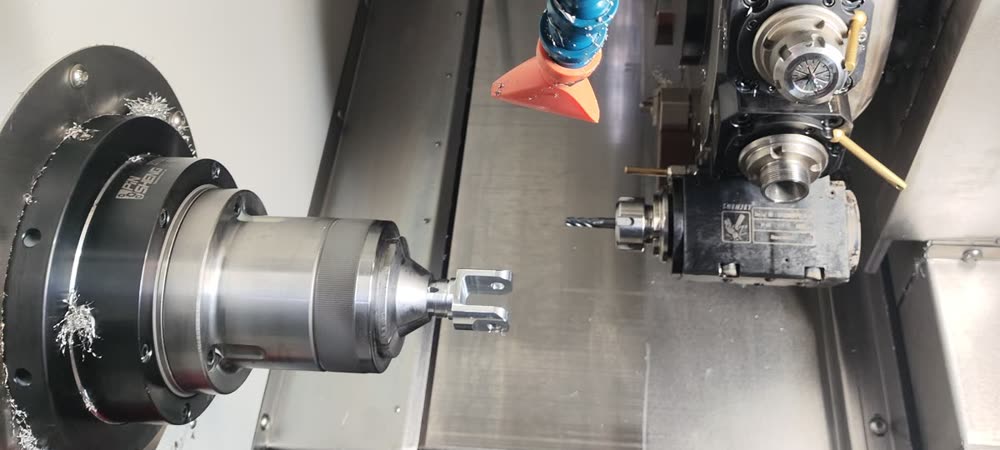
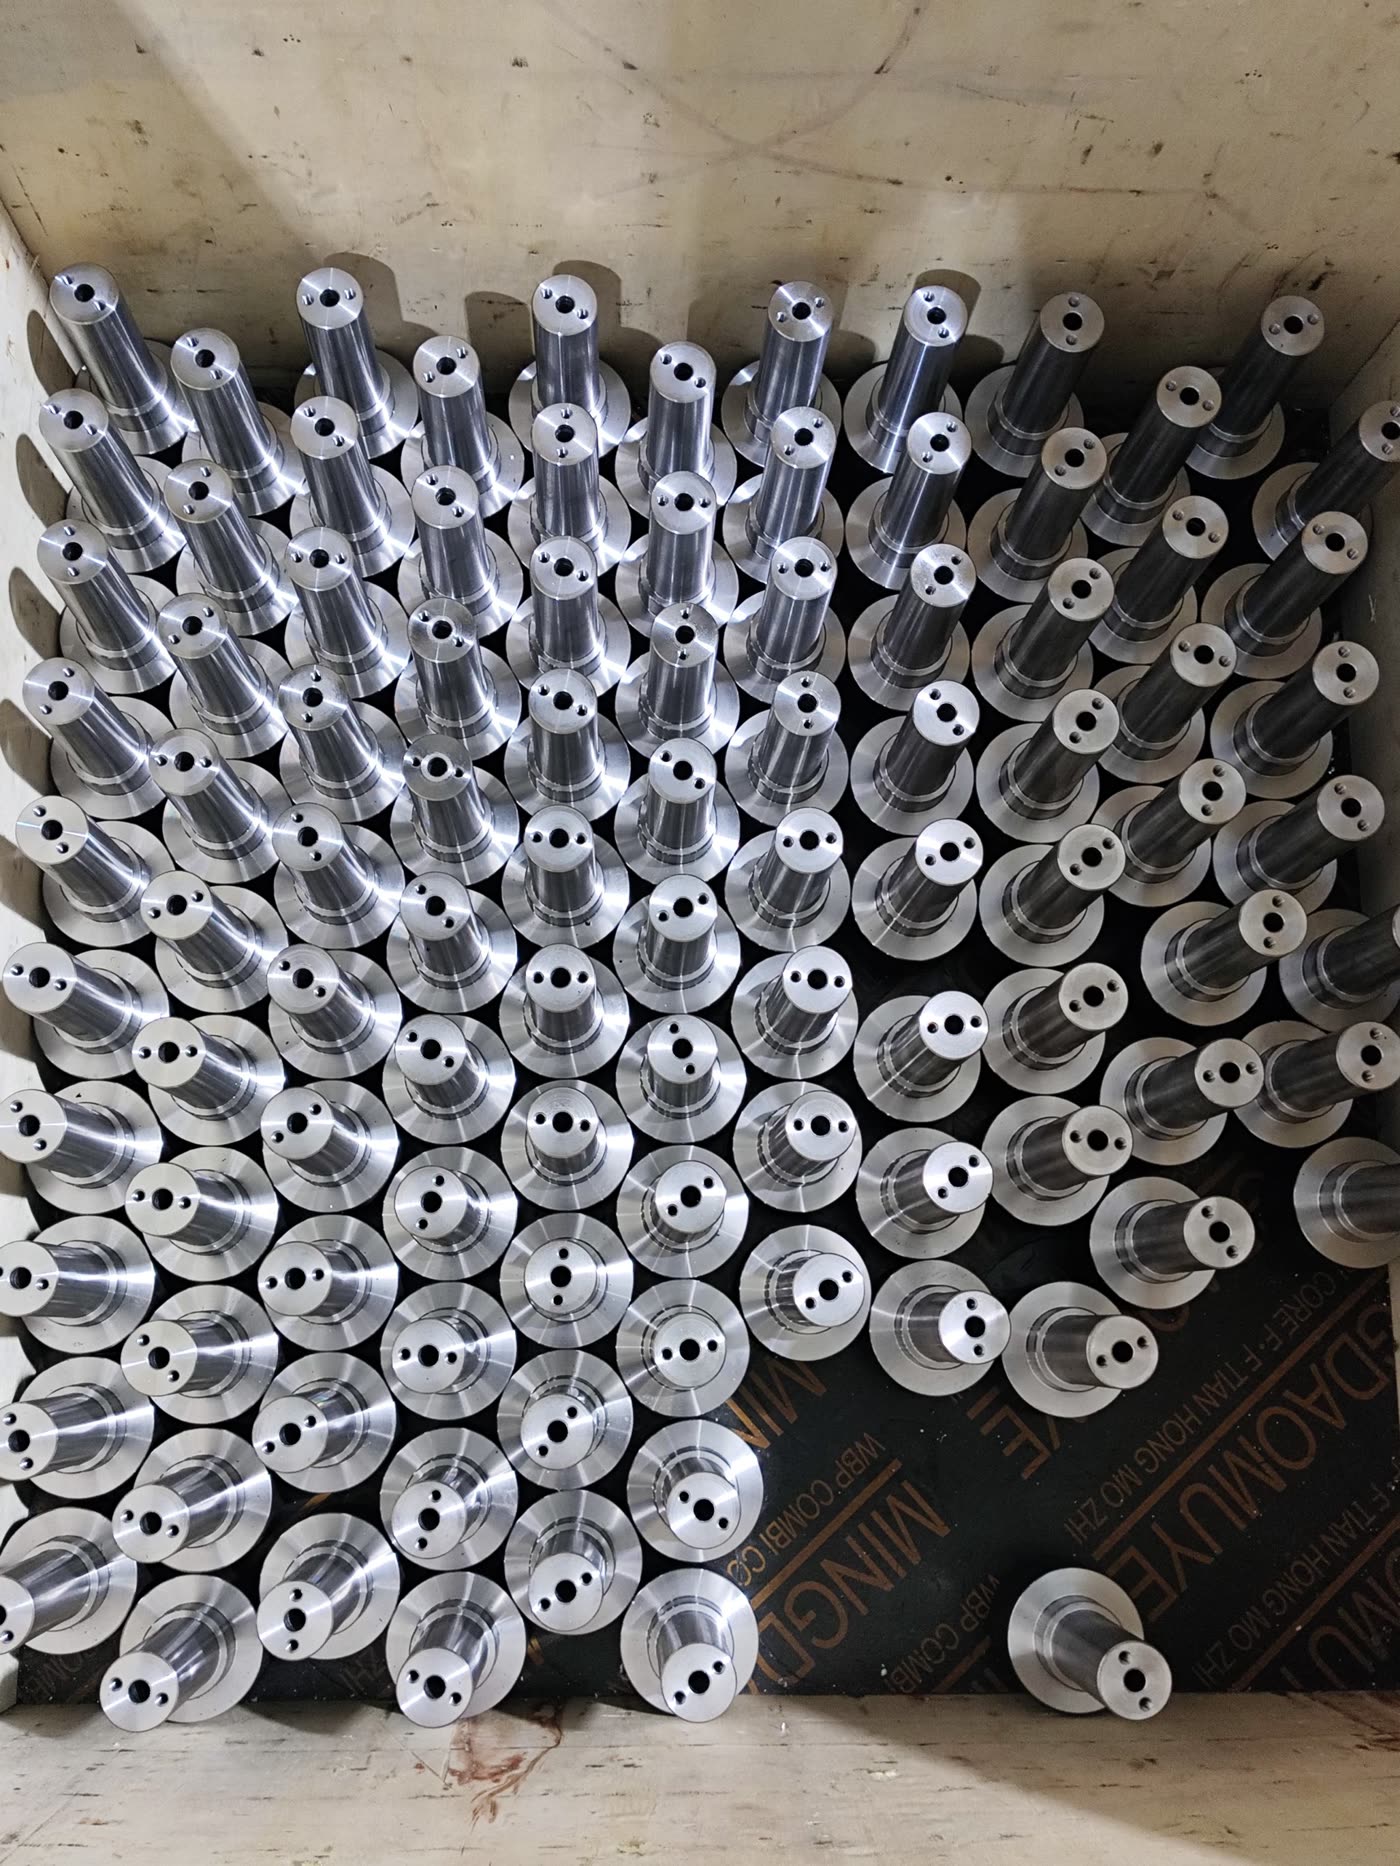
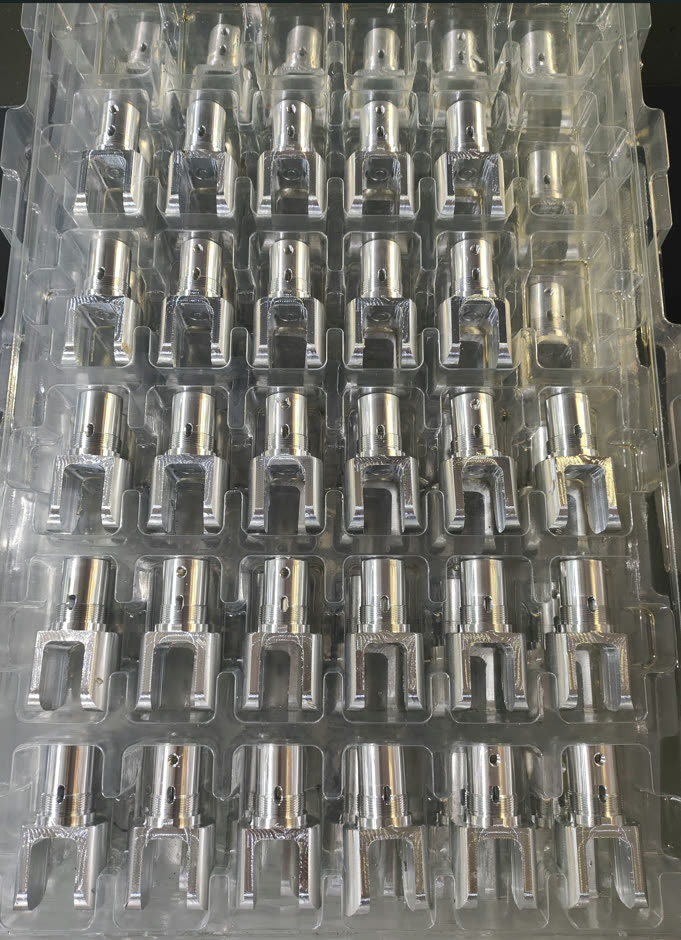
Some parts are turned, then milled, then turned again — every re-clamp is a chance to lose accuracy. Mill-turn does it in one setup: the shaft is turned, the flats and cross holes are milled, and the part comes off finished.
Concentricity between the turned and milled features is held by the machine, not by luck. It is the right route for valve parts, connectors, stepped shafts with wrench flats, and sleeves with side ports.
Typical parts
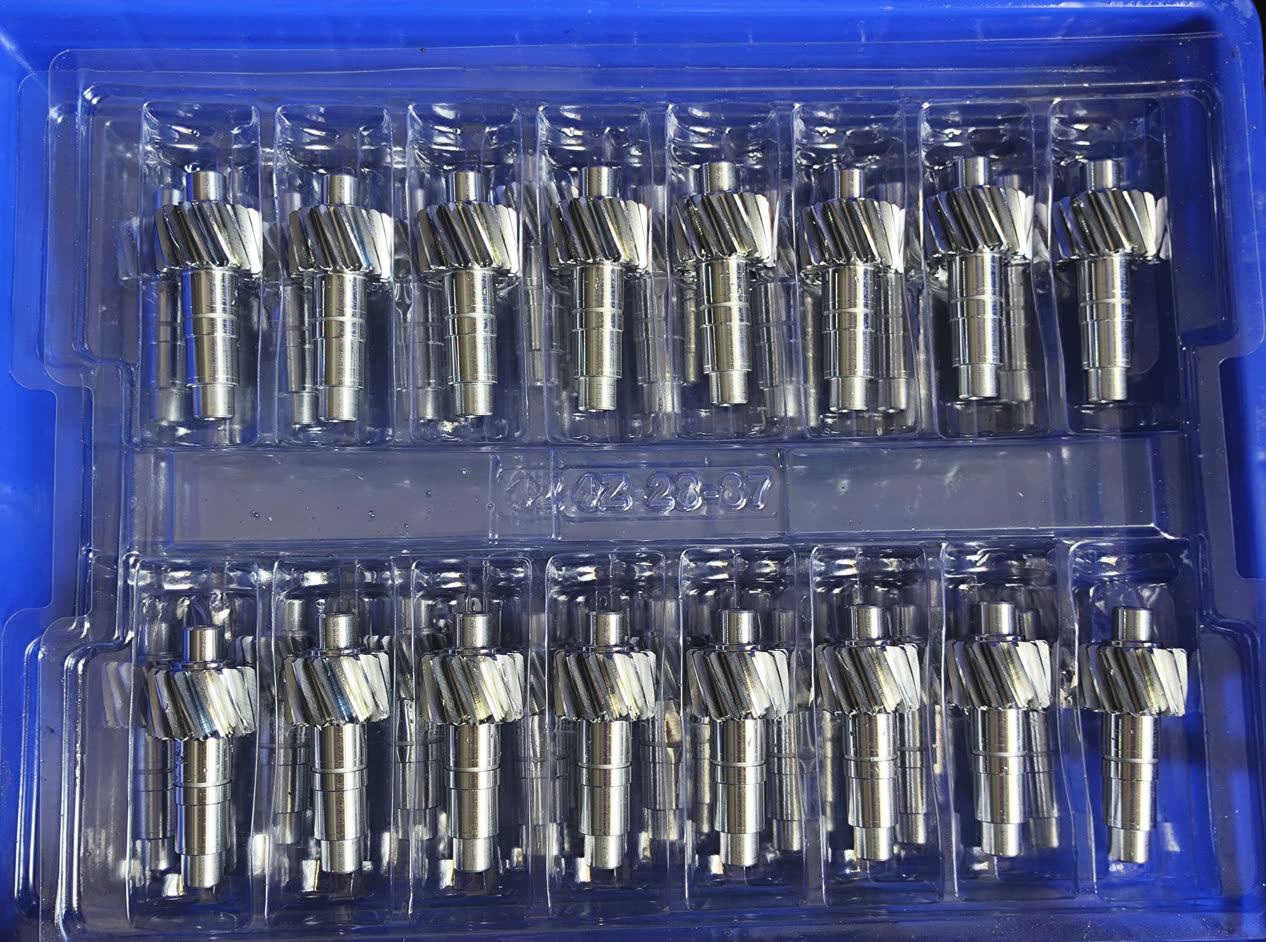
Stepped shafts with flatsSleeves with cross holesValve componentsFittings & connectors
We will tell you honestly if mill-turn is the cheapest route — or if plain turning does the job.
| Tolerance | To ±0.005 mm |
|---|---|
| Live tooling | Cross drilling, milling flats, slots |
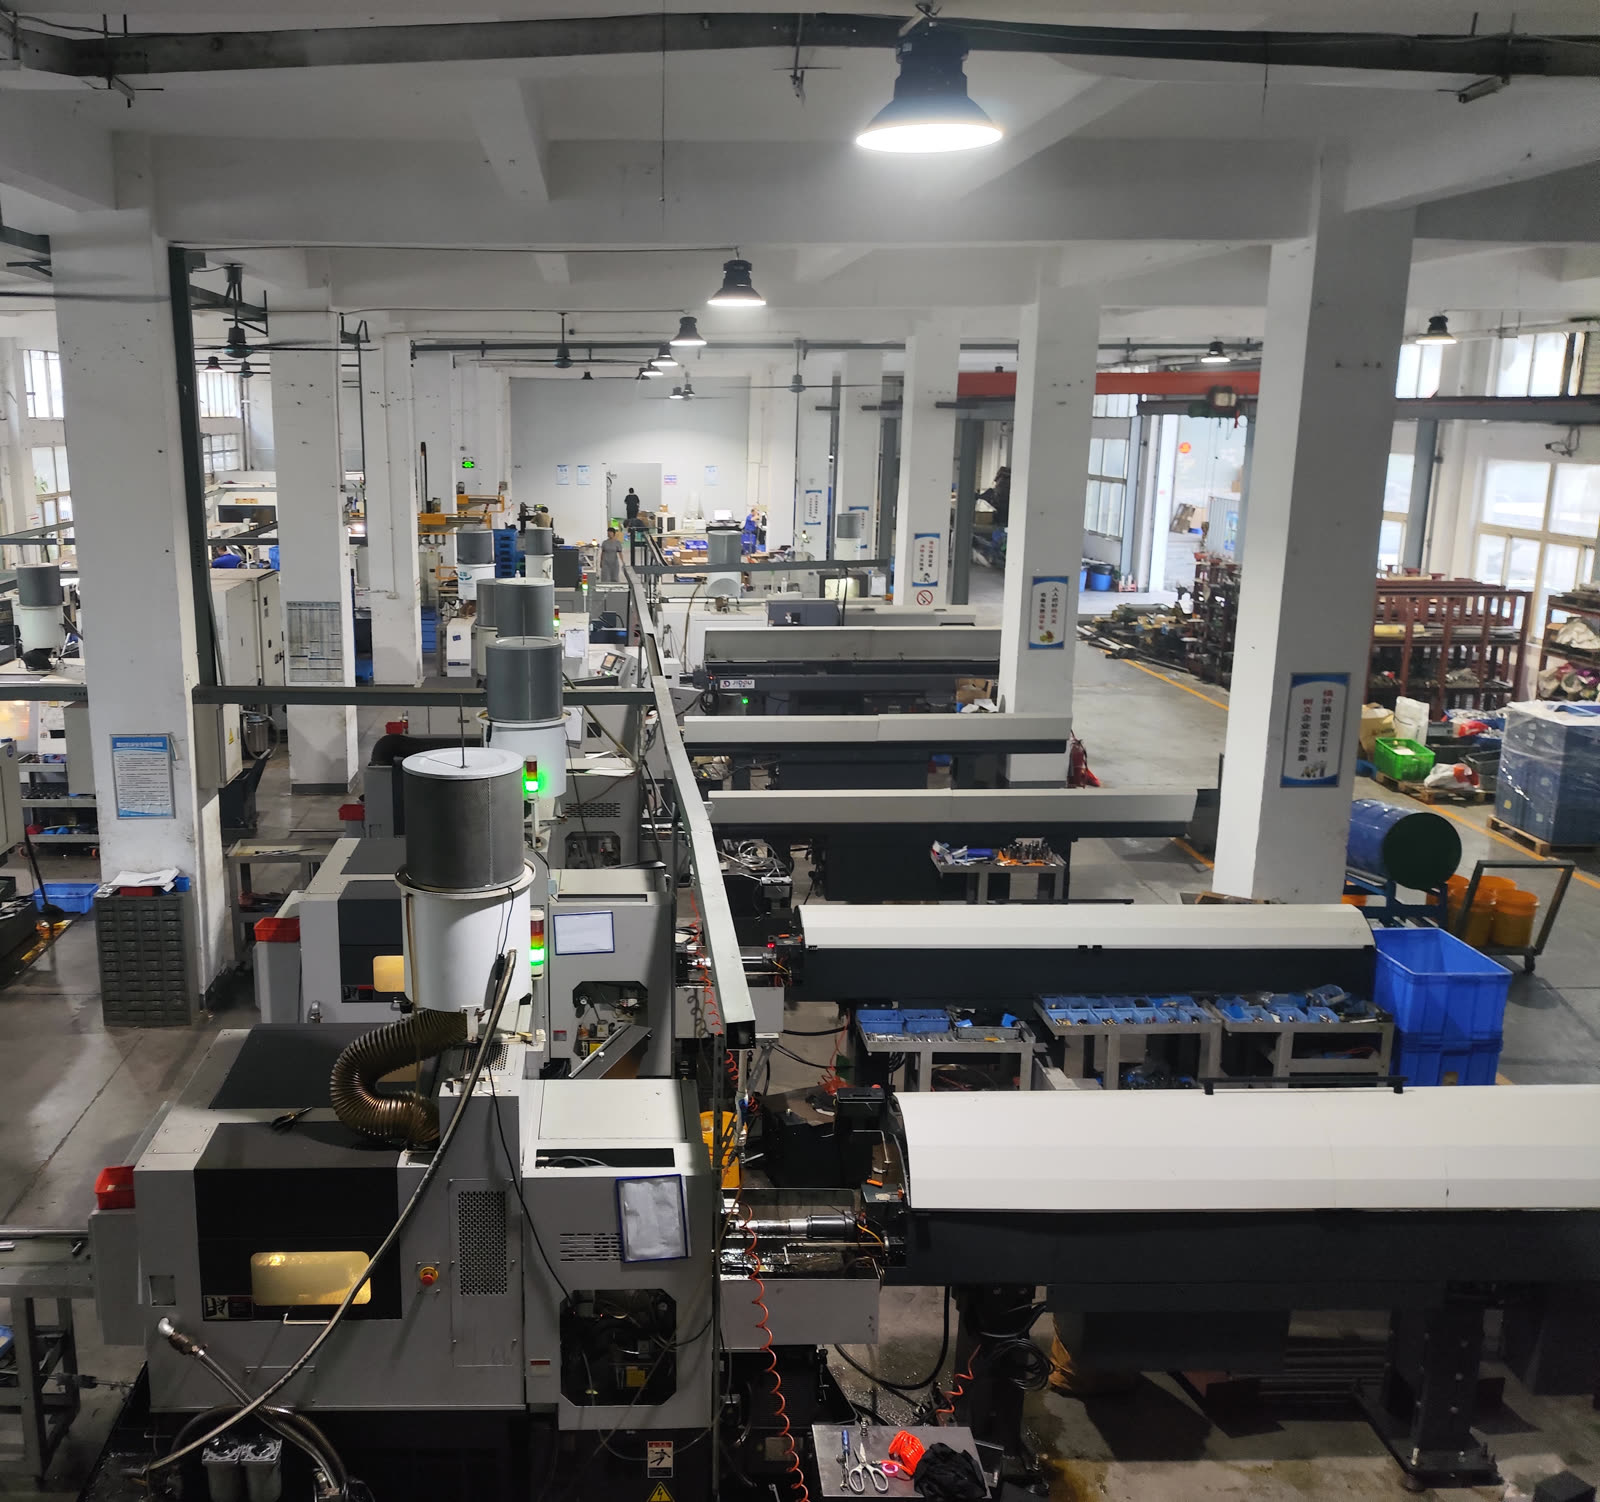
| Orders | Prototype and batch production |